
Technologist & Leader
Hi, I'm Justin Hall.
This is my little corner of the internet — not a portfolio, just a place to share who I am outside of work.
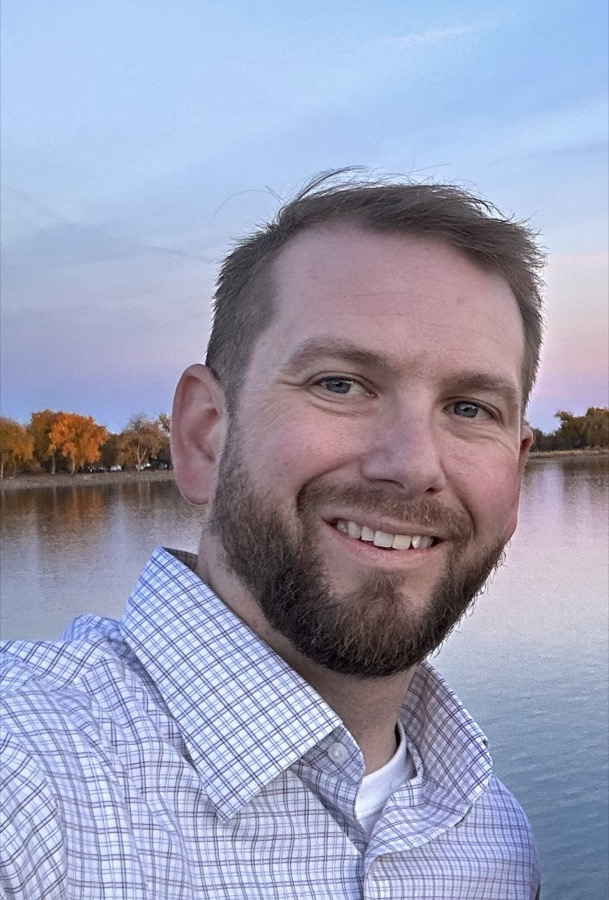
About Me
My kids have moved on to full-time coaches now, so after years on the soccer field and hockey rink, I've traded the sideline for a private range and a garage full of half-finished projects. Although I still enjoy flying around the country to watch my son play hockey or catch up with my daughter at school.
I'm back in school myself — partway through an MBA and a Master's in Business Analytics at the University of Iowa, on track to finish in 2027. I'd rather be the person in the room who is still learning something than the one who has decided he's done.
What I Do
I started with a B.S. in Electrical Engineering Technology from the University of Northern Iowa, and I've spent about fifteen years since then in manufacturing — maintenance, operations, and the engineering work that sits in between.
Most recently I led the biggest project our foundry has taken on in fifteen years — automating molten-iron delivery and pouring. Cold-shut defects dropped over 90%, throughput went from 34 to 45 castings an hour, and training new operators went from six months to a single day. Read the writeup →
As of June 2026 I moved into a Business Transformation Lead role — designing our foundry's 10-year plan. Most of my attention these days goes to AI, robotics, and automation, and closing the gap between a good demo and something that still works on second shift in February.
Started here as a Factory Automation Engineer — PLC programming, SQL/database, and VB work across the 804 & 871 lines, including building the foundry's current report-manager website.
Things I'm Into
- Target shooting at a private range.
- Handyman projects in the garage — there's always something torn apart out there.
- Home automation and other techy side projects.
- Volunteering with STEM programs at Waterloo Elementary School.
- Keeping a foot in IEEE, AFS, and ASEE.
Pour the Iron
Before Autopour, a crew filled the molds by hand — about 34 castings an hour. A ladle gets charged with molten iron at the furnace, walked out to the mold line, poured down into the molds one at a time, and walked back to be charged again. Every trip back is time the line is not being poured.
The pour itself is aiming a stream of iron into a hole a few inches across in the top of the mold, with the whole ladle hanging off a crane that keeps swinging after you stop. Three things come out of a bad one. A cold shut is an interrupted pour: the iron already in the mold freezes over on top, and when the stream comes back the new metal lays over that skin instead of fusing to it, leaving layers straight through the casting. A cold-shut casting can be full to the top and still be scrap. A short pour is literally a short casting — the mold never got filled all the way. A runout is when the mold splits and the iron ends up on the floor — that one is the mold line's fault and nobody's error.
Automating the delivery and the pour took the walking out of it: the ladle never leaves the line. The line holds 45 castings an hour now, and cold shuts dropped over 90%.
Want to try pouring iron? →
The interactive version needs JavaScript. The numbers above are real either way.
On the mold line
Open this and press Space to start a shift.
Say Hello
The best way to reach me is jd9hall@gmail.com. I read everything that comes in, and I answer most of it. I'm also on LinkedIn.
Ask AI About Me
Curious what an AI assistant says about me? Pick a question, then ask one directly.
I use these tools deliberately rather than interchangeably — here's how I split the work between them.